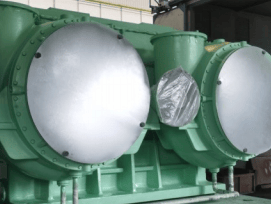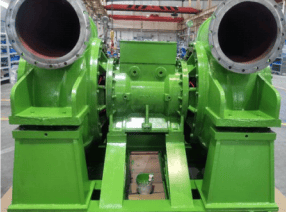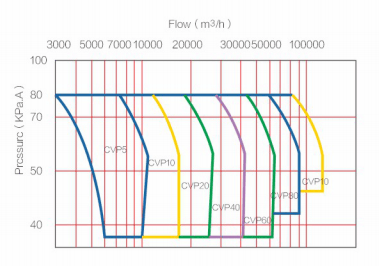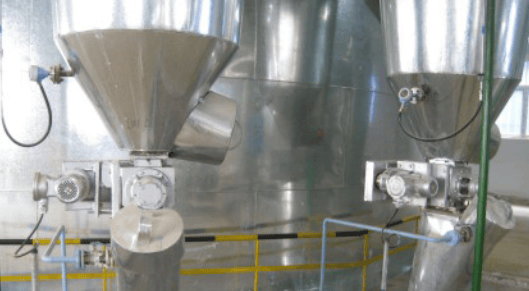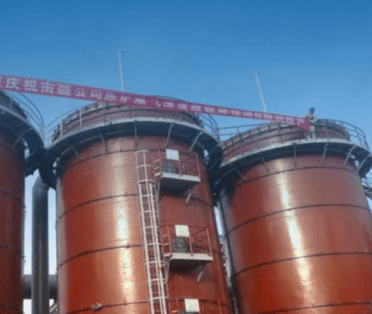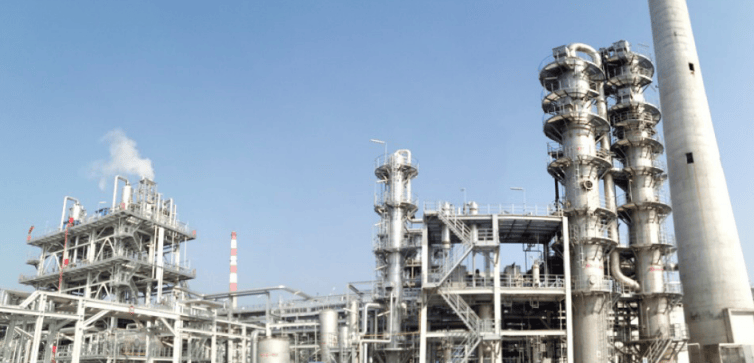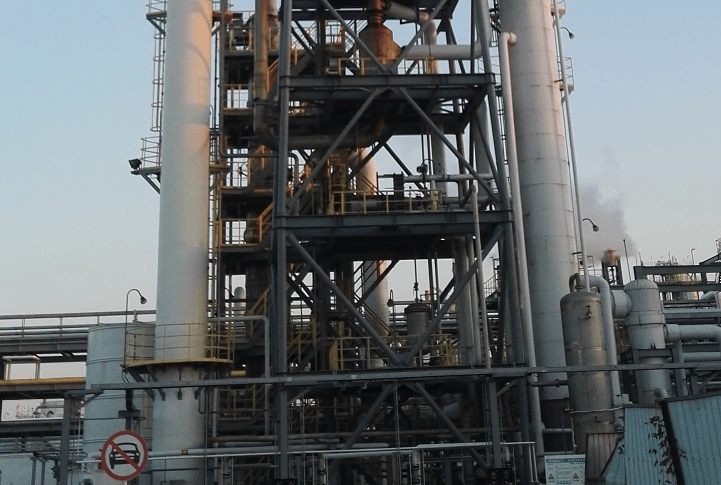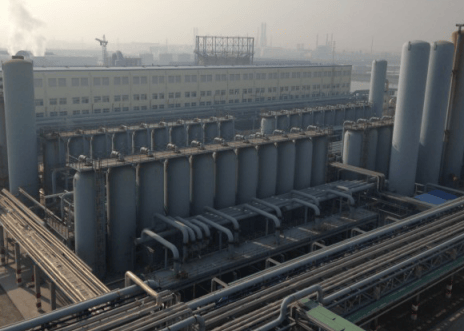

Flue gas from different sources, with varying concentrations, humidity levels, and impurity compositions, first undergoes dust removal, cooling, and pressure boosting before entering a deep purification tower group, where impurities such as H₂O, SO₂, and NOx are adsorbed through the selective adsorption of different adsorbent combinations. The purified gas exiting from the top of the deep purification tower is pressurized and then enters a PSA adsorption tower group consisting of one or more stages of combined multi-tower units for enrichment, where CO₂ is adsorbed by the adsorbent, while non-adsorbed components such as N₂, O₂, and CO are discharged from the top of the PSA adsorption tower. After the adsorbent becomes saturated with CO₂, CO₂ is desorbed under vacuum by a vacuum pump, then cooled, compressed, and fed into a TSA purification tower to further remove trace impurities and moisture, thereby obtaining high-purity CO₂ gas with a concentration of >98%.
The PSA adsorption and regeneration process consists of steps including adsorption, pressure equalization and depressurization, reverse depressurization, vacuum extraction, pressure equalization and pressurization, and product gas pressurization.
The high-purity CO₂ gas produced by the PSA unit, when combined with low-temperature liquefaction, rectification purification, and other facilities, can be used to produce industrial-grade and food-grade liquid CO₂ products, or CO₂ gas products for various applications.
Technical Features
• The PSA flue gas CO₂ recovery process is advanced, simple, and has a short flow, overcoming the drawbacks of periodic liquid heating and cooling in wet decarbonization processes.
• The low-pressure PSA process is adopted, significantly reducing energy consumption and investment.
• The unit has strong adaptability. For various flue gases with CO₂ concentrations ranging from 15% to 80%, complex impurity compositions, and large fluctuations in humidity, pressure, and flow rate, it demonstrates strong adaptability through different process combinations and the selection of suitable adsorbents.
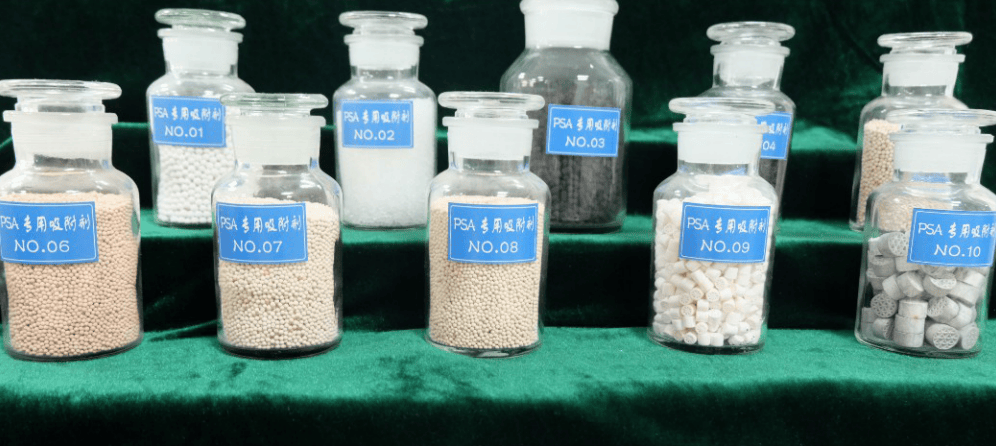
• Specialized adsorbents developed by Huaxi are used, featuring strong purification capacity and high purification degree. CO₂ gas purity can reach over 98%, with a high CO₂ recovery rate.
• The unit has a high degree of automation and flexible operation. The PSA system can automatically switch towers for online troubleshooting.
• The unit starts quickly with a short startup cycle. Typically, product can be obtained within 30 minutes of startup. The equipment technology is mature, reliable in operation, has a long service life, and requires minimal maintenance.
• The unit discharges no wastewater, and the exhaust gas does not increase the total amount of pollutant emissions.
Applications
• Decarbonization or CO₂ recovery in fields such as lime kiln gas, converter gas, blast furnace gas, boiler flue gas, dry quenching circulating gas, and ironmaking hot blast stove flue gas.
• Industrial-grade and food-grade carbon dioxide production.