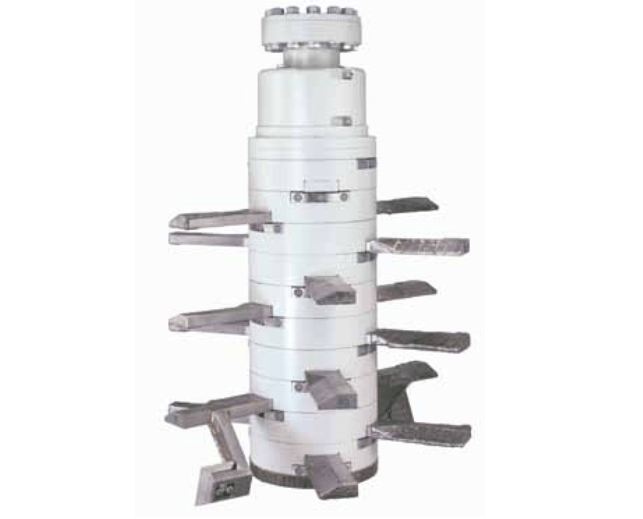
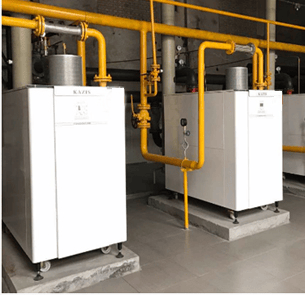

The inverted full premixed ultra-low NOx condensing boiler is a general term for ultra-low NOx boilers that adopt full premixed technology and high calorific value condensing technology. The condensing technology used in condensing boilers can recover and utilize the residual heat in flue gas, and the combustion mode is full premixed proportional regulation. The flue gas exhaust temperature of condensing boilers can be reduced to approximately 35°C, and the latent heat of water vapor in the flue gas can be absorbed and utilized. For this reason, the efficiency can reach as high as 109%. Surface combustion technology is adopted during the combustion process, making combustion more thorough, resulting in lower energy consumption and better environmental performance of condensing boilers.
Product Features
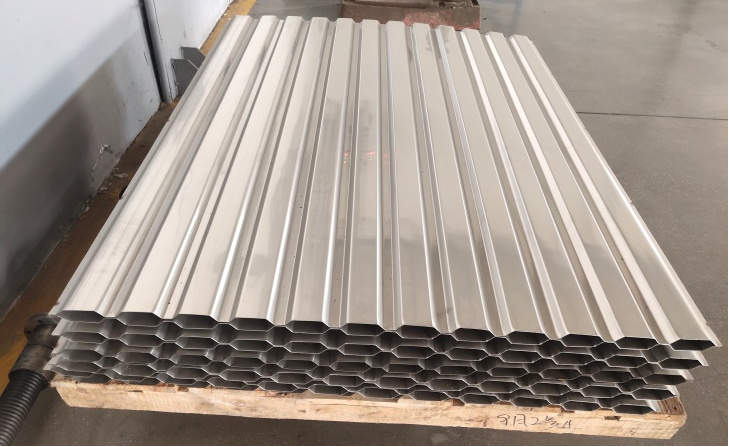
1. The entire unit is designed and manufactured by our company, with quality assurance: stainless steel heat exchanger with strong corrosion resistance; German SIEMENS controller with Class III output commands and output signals; 11 layers of protection in the execution process to ensure combustion conditions without hidden risks; stepless variable frequency adjustment function to enhance user experience.
2. Pressure-bearing boiler, atmospheric operation: primary closed-loop system operation, water pressure of 1~4 kg, managed as atmospheric operation.
3. Energy-saving and environmentally friendly, excellent quietness: full premixed combustion technology and condensing heat exchange technology, thermal efficiency reaches 109%; ultra-low nitrogen oxide emissions can be minimized.
4. Quiet combustion, below 45dB: the temperature difference between flue gas temperature and boiler return water reaches 3-5°C, and the exhaust temperature is as low as 35°C, striving to create a green lifestyle.
5. Intelligent control, Chinese interface: reserved MODBUS RTU communication interface, which can be matched with building automation systems to achieve remote intelligent control. Meanwhile, the SIEMENS screen is equipped with a Chinese human-machine interface, which is simple and convenient.
6. Space-saving, short project duration: compact body with large capacity, can adopt stacked structure. The floor area of a single 1-ton boiler is only 1.6㎡, and the installation period is 1~2 days.
Multiple Protections
1. Safety valve: a protection system to prevent boiler overpressure.
2. Automatic exhaust valve: automatically removes air from the boiler.
3. Flue gas sensor: monitors flue gas temperature to prevent overheating; if the flue gas temperature exceeds 85°C, the system alarms.
4. Frost protection: automatically activated based on the readings of the frost protection sensor on the boiler. The automatic frost protection device remains in operation to prevent frosting (the boiler must be in standby mode).
5. Pump seizure protection: when the boiler is not in use for a long time, the pump will emit a 5-second pulse every 24 hours to keep the pump running, thereby avoiding blockage caused by oxygen corrosion.
6. Flame detection electrode: continuously monitors the burner flame; if there is no flame, the gas inlet valve will be closed to protect the system.
7. Combustion pressure monitoring: low gas pressure and low air pressure alarm, extremely low pressure boiler shutdown protection.
8. Boiler pressure monitoring: continuously monitors boiler pressure; if low water pressure or excessively high water pressure occurs, the system will stop operating.
9. Boiler over-temperature protection system: if the boiler temperature exceeds 95°C, the burner stops operating.
10. Boiler secondary temperature protector: if the water flow temperature exceeds 105°C, the system will stop operating.
11. High/low voltage protection: protects the boiler when there is a voltage problem.
Specification Options
Currently, 100KW, 200KW, 300KW, 400KW, 500KW, 700KW, 1000KW, and 1400KW are available for users to choose from.